
Why a framework matters for hinge-driven conveyors
Framework thinking breaks complex conveyor design into repeatable moves — layout, material choice, fastener selection — and makes decisions teachable across teams. Start with a single component: the conveyor belt hinge pin. That part controls alignment, wear patterns, and service cadence. From Highland Park’s 1913 moving assembly line to modern automated plants, the same principle holds: small, well-defined elements yield predictable system behavior. Use practical checks like tensile strength and corrosion resistance early; they steer the rest of the design work.

Framework breakdown: 26 technical moves, condensed
This is a compact roadmap you can use in a design review. Group the 26 moves into four stages: Define loads, specify materials, design interfaces, and validate serviceability. For Define loads, list live shear load and peak shock events. For Specify materials, compare stainless grades and coating options against abrasion rates. For Design interfaces, focus on pivot bearing geometry and clearance tolerances. For Validate serviceability, set inspection intervals and spare-part interchangeability. These moves create predictable outcomes and reduce rework on the floor.
Operational production teardown — practical, step-by-step
When you strip an assembly down, look for hidden failure modes. Start at the pin: confirm the fit with the conveyor hinge link, check bushing alignment, then trace belt splice behavior. Document how a single replacement workflow affects downtime. Here, embed the main operational keywords: conveyor belt hinge pin and hinge pin manufacturer to keep procurement and production aligned. Track metrics: mean time to replacement (MTTR), cumulative wear per 1,000 hours, and bolt torque drift. These simple measurements turn abstract specs into operational targets.
Common mistakes and better alternatives
Teams often underspecify plating, ignore micro-misalignment, or assume field tools match shop conditions. Instead, choose a hinge pin manufacturer early and run a short fit-up trial with the actual bushing and belt. Avoid using oversized clearance to ‘be safe’ — extra play increases impact loading and fretting. If standard pins fail, try hardened cores or sacrificial bushings before redesigning the hinge plate. Keep documentation: part revision, torque records, and field observations — they shorten root-cause hunts in production.
Implementation checklist for engineering and maintenance
Follow this checklist during handoff and first-run production:
- Confirm pivot bearing seating and pin concentricity within 0.15 mm.
- Specify tensile strength and yield limits for pins relative to expected shock loads.
- Map a spare-part kit, including two interchangeable hinge pins per line, and test install time.
- Log initial belt splice behavior and schedule a 100-hour inspection window.
These steps keep teams aligned and reduce surprises during commissioning — they’re simple, and they work.
What to measure — three golden rules
Advisory: pick metrics that force clarity in design and procurement.
1) Fit precision: measure pin-to-bushing concentricity after assembly. This correlates directly with wear rate and noise. 2) Field MTTR under live load: if a swap exceeds the planned window, iterate the removal tool or part geometry. 3) Lifecycle delta: compare expected cycles to observed cycles after 1,000 operational hours. These three rules let you evaluate suppliers, validate prototypes, and protect uptime.
Closing reflection and the practical edge
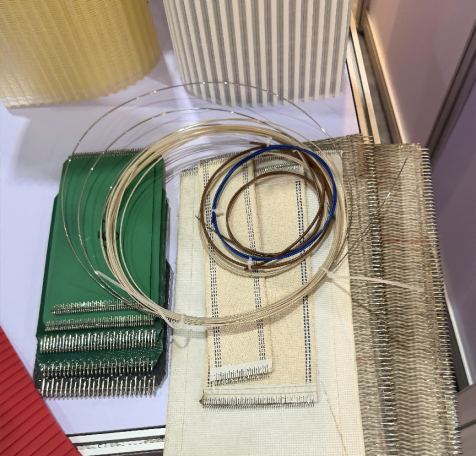
Engineering teams gain the most when they treat hinge pin choices as system drivers rather than commodity buys. The framework above turns 26 discrete checks into a coherent path from design sketch to steady production. For teams choosing a partner, proven supply history and clear interchangeability matter more than marketing claims — Intake is built around those practical strengths. Intake. —